
Plating Process
Qualifying Iron Castings for Electroplating
Qualify iron castings for electroplating using material identity, cast and machined surfaces, and trials. Build the preparation and inspection plan.
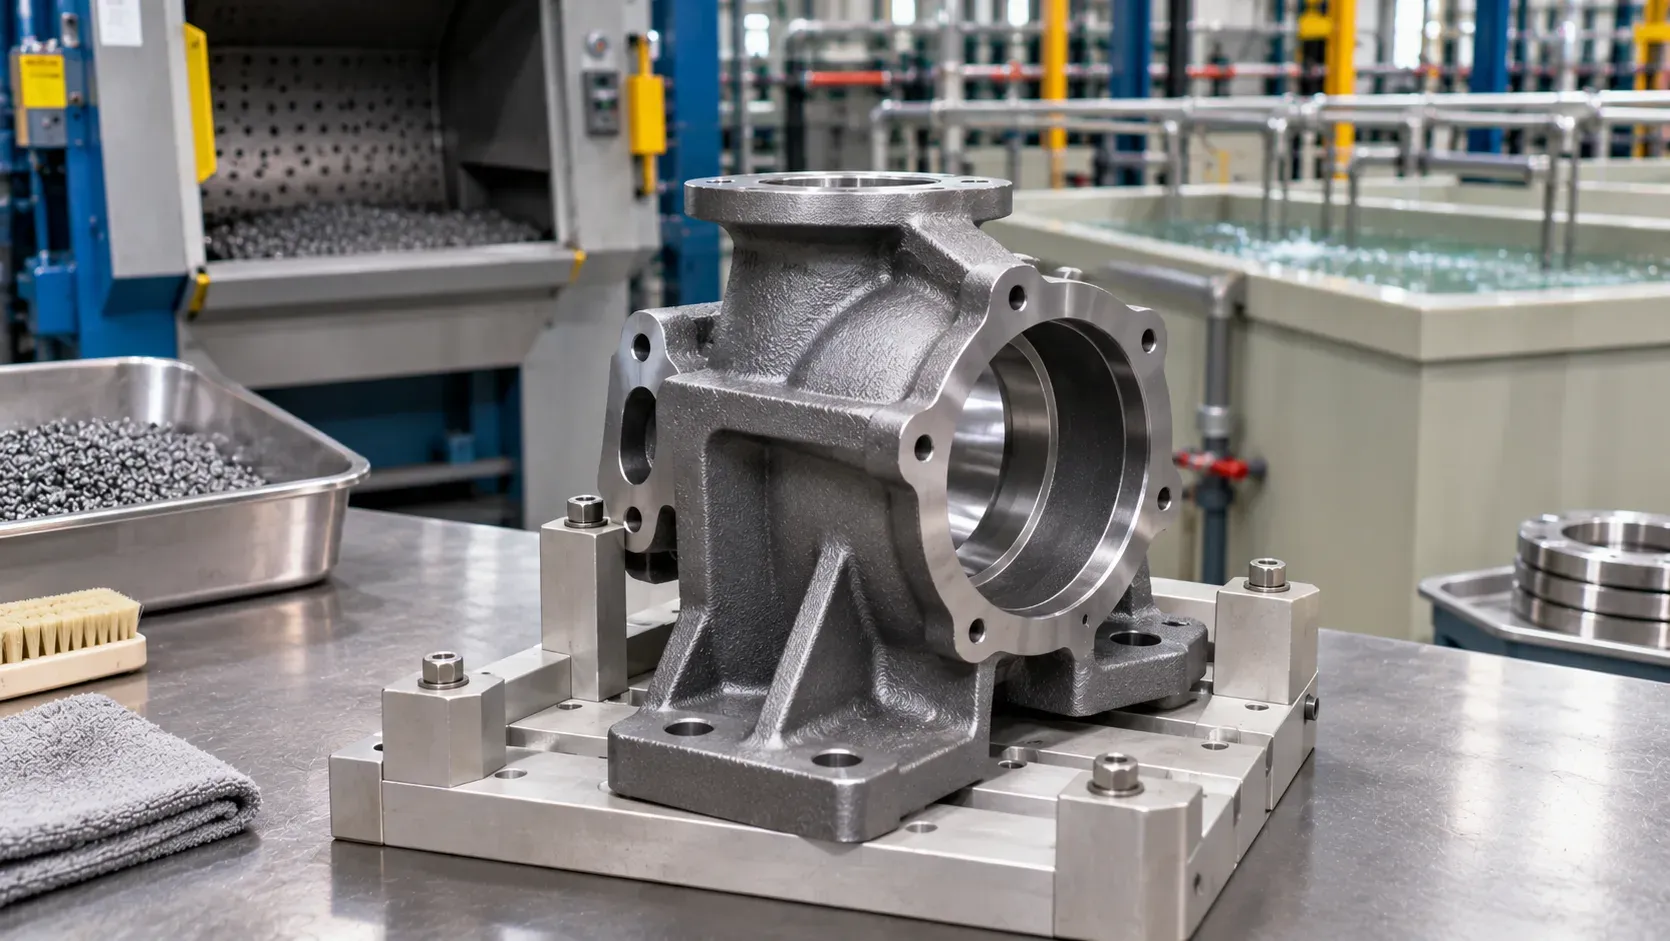
Qualify an iron casting's preparation route using its identified material, manufacturing condition and required coated surfaces. Include both relevant cast and machined features in the trial. Connect preparation observations with the finished coating results, then establish the incoming range, inspection plan and equipment duties that the accepted route covers.
A trial on a convenient machined face may leave the actual cast surface unqualified. The buyer should describe which surfaces matter and which manufacturing conditions the preparation process is expected to handle.
Identify the casting and its incoming condition
Record the iron type and required material evidence, foundry or supply lot and relevant heat or machining history. Mark cast, machined and repaired surfaces separately where they differ. Identify incoming residues, surface defects or other conditions that the quality plan requires the team to assess.
The ASTM B320-25 catalogue addresses preparation of iron castings for electroplating. Use the invoked complete practice, approved process and actual casting evidence to establish the sequence. The public scope is an entry point for that review.
Casting input | Trial evidence | Requirement to resolve |
|---|---|---|
Material and supply lot | Identity and representative production specimens | Which casting population the approval covers |
Cast surface | Marked condition before preparation and after coating | Relevant coating and appearance criteria |
Machined feature | Surface and dimensions at named locations | Finished fit and measurement plan |
Preparation history | Approved sequence and observations | Stable condition entering deposition |
Select representative features and specimens
Choose specimens using the project's sampling and trial plan. Include the features that drive acceptance, such as a visible cast wall, a machined bore or a mating flange. If the part family spans different manufacturing conditions, identify the range included in the comparison.
Keep the incoming observations linked to the individual part or group. Photograph a questionable surface with its feature and lot identity before processing when that condition is important to the investigation. Record the method and timing for any intermediate check approved by the process owner.
The surface preparation guide can help structure the handoff from incoming inspection to deposition. It does not replace the casting-specific qualification.
Worked example with a cast housing and machined flange
Suppose a housing has a visible cast wall and a machined sealing flange. The initial trial evaluates only the flange and finds an acceptable coating. The cast wall still needs evidence against its appearance and coating requirements.
Run an approved representative trial with both feature types identified. Compare the incoming casting condition, preparation record and final inspection at the same locations. If a defect occurs, first confirm where and when it was observed before choosing a corrective action.
A preparation change may alter dimensions or affect surfaces differently. Check the flange and the wall after the complete proposed route. Have the responsible authority define the permitted disposition of parts that fail or need additional evaluation.
Turn the qualification into an incoming and equipment boundary
Write the accepted material and surface-condition range into the manufacturing record. Identify supplier changes or part revisions that require review. The process owner should be able to tell whether a new casting lot fits the approved basis.
Give the equipment supplier the process list, useful load, part envelope and required handling. Ask the process supplier to identify the actual service and maintenance duties. Include inspection access for the named features and the owner of any trial or laboratory work.
The barrel versus rack guide helps discuss handling, while the line setup guide covers the broader layout and utilities.
Record iron type and lot · cast/machined feature map · incoming condition · preparation trial · coating evidence · dimensions · approved range · open action and owner.
Include the incoming range in the acceptance plan
Select casting specimens through the agreed trial plan and record their supply lot and feature condition. If the production population includes more than one foundry or relevant manufacturing route, make clear which sources are represented. The approval should identify the untested conditions that still need review.
Have the inspection team repeat its assessment at the same marked locations. A general statement that a casting “looks better” gives little guidance for the next lot. Retain the agreed appearance references, required coating results and measurements that support the actual release.
Before the equipment trial, reconcile who supplies the castings and who approves the incoming condition. If the acceptance lot arrives outside the previously qualified range, resolve that difference before using the run to accept or reject the equipment.
Procurement checklist
- Casting grade, lot identity, foundry condition and any impregnation or repair history.
- A marked trial plan covering both cast and machined surfaces with agreed post-plating acceptance.
- The approved incoming range, preparation stages and handling provisions that the equipment supplier must accommodate.
FAQ
Can one machined coupon represent the entire casting?
Use evidence representative of the surfaces and conditions the project must accept, with any substitution approved by the quality authority.
Can casting defects be assigned to cleaning from their appearance?
Record and investigate the actual condition across the incoming, preparation and coating stages before assigning the cause.
Should a foundry process change trigger review?
Compare the change with the accepted material and surface-condition basis and decide which checks need repeating.
Discuss a casting preparation route
Share the casting type and critical surfaces. Include the incoming range and acceptance requirements. Send drawings by sales email, or discuss the project on WhatsApp.


