AMS2404 covers electroless nickel-phosphorus plating. Identify the contract revision, deposit requirements, substrate, final condition and acceptance evidence before specifying tanks or ovens. A standard designation is an assessment input, not proof that a line or supplier is approved.
In this guide
What does AMS 2404 require for electroless nickel plating?
The SAE page for AMS2404K identifies the coating family and revision. Its public scope does not reproduce every classification, default or inspection clause.
Provide the contract revision and relevant drawing or purchase-order requirements. Confirm thickness and measurement locations, specified deposit composition, final condition, substrate restrictions and quality flow-downs. Resolve omissions or conflicts with the responsible authority.
Distinguish requirements transcribed from the controlled standard from choices awaiting approval. Do not assume a class default, phosphorus range or historic thickness rule without checking the applicable edition.
Which thermal duties must an AMS 2404 line brief distinguish?
Treat class selection as a controlled-document decision. SAE's public AMS2404K page verifies the coating family and October 2024 revision, but it does not expose the full class table. This equipment guide therefore does not reproduce class numbers, defaults or numerical heat-treatment schedules. Transfer the invoked class and approved schedule from the contract edition into the line brief.
The following is an equipment-duty checklist, not an AMS classification table:
| Required final-condition duty | Question for the process authority | Equipment and evidence to define |
|---|---|---|
| No property-changing post-treatment | Is this the approved final condition, and do any separate relief requirements remain? | Drying scope, any separate bake and the inspection stage |
| Deposit hardening | Which approved treatment produces the required deposit property without harming the substrate? | Working envelope, load pattern, approved temperature/time control and property test |
| Adhesion-improvement treatment | What substrate and approved treatment apply? | Oven duty, load identification and adhesion evidence after the required treatment |
| Hydrogen-embrittlement relief, if applicable | Does the material and contract require a separate duty or an approved combined route? | Sequence/timing responsibility and traceable treatment record |
Drying removes retained moisture; it does not by itself demonstrate deposit hardening, adhesion improvement or embrittlement relief. An oven quoted without the approved duty, usable load envelope, controls and records is an unresolved scope item. The process authority must resolve substrate temperature limits and any required equipment qualification before selection.
Which acceptance records should an AMS 2404 plating job produce?
Build a requirement-to-evidence matrix with the quality owner. It can include approved process records, thickness locations, adhesion checks, final-condition measurements and thermal-treatment records where applicable. Identify the governing clause, specimen, frequency, acceptance rule and responsible party.
ASTM B571 describes qualitative adhesion practices; it is not automatically the required method for every AMS job. Use the selected method only where the contract or responsible authority invokes it.
Distinguish supplied monitoring and record-export functions from laboratory services and approvals. Request a sample record format and a representative-load demonstration against the agreed matrix.
Example: turning a thickness callout into a traceable record
This is an illustrative buyer worksheet, not an AMS acceptance limit or a customer result:
| Matrix field | Example entry or action |
|---|---|
| Requirement identity | Actual drawing number/revision and coating note, plus the invoked AMS edition |
| Location and condition | Mark each measurement point on the part drawing; identify the final inspection stage |
| Method | Quality owner selects a method suitable for coating, substrate, geometry and required range |
| Recorded evidence | Part/lot and load IDs, point map, instrument ID, calibration/check status, actual readings and operator/date |
| Acceptance reference | Link to the approved drawing/specification clause; do not let software invent a tolerance |
| Ownership | Equipment supplier identifies included measurement/export functions; processor records the job; authorized quality personnel decide acceptance |
Ask for a demonstration that retrieves one agreed lot's readings and applicable process records. A temperature trend alone is not a thickness report, and an instrument export alone is not a conformity decision.
What belongs in an AMS 2404 electroless nickel line brief?
| Input | What to provide | What the proposal should clarify |
|---|---|---|
| Callout | AMS revision, class, drawing thickness, phosphorus requirement from the process owner | Process route and control points |
| Substrate | Alloy, condition, heat-treatment state | Pretreatment sequence and material assumptions |
| Post-plating | Required thermal treatment per class | Oven scope, profiles and records |
| Acceptance | Thickness locations, adhesion method, inspection plan | Instruments, specimens and record format |
| Volume | Part families, loading method, production schedule | Load size and throughput basis |
| Documentation | Contract and quality-flow-down requirements | Included records and responsible parties |
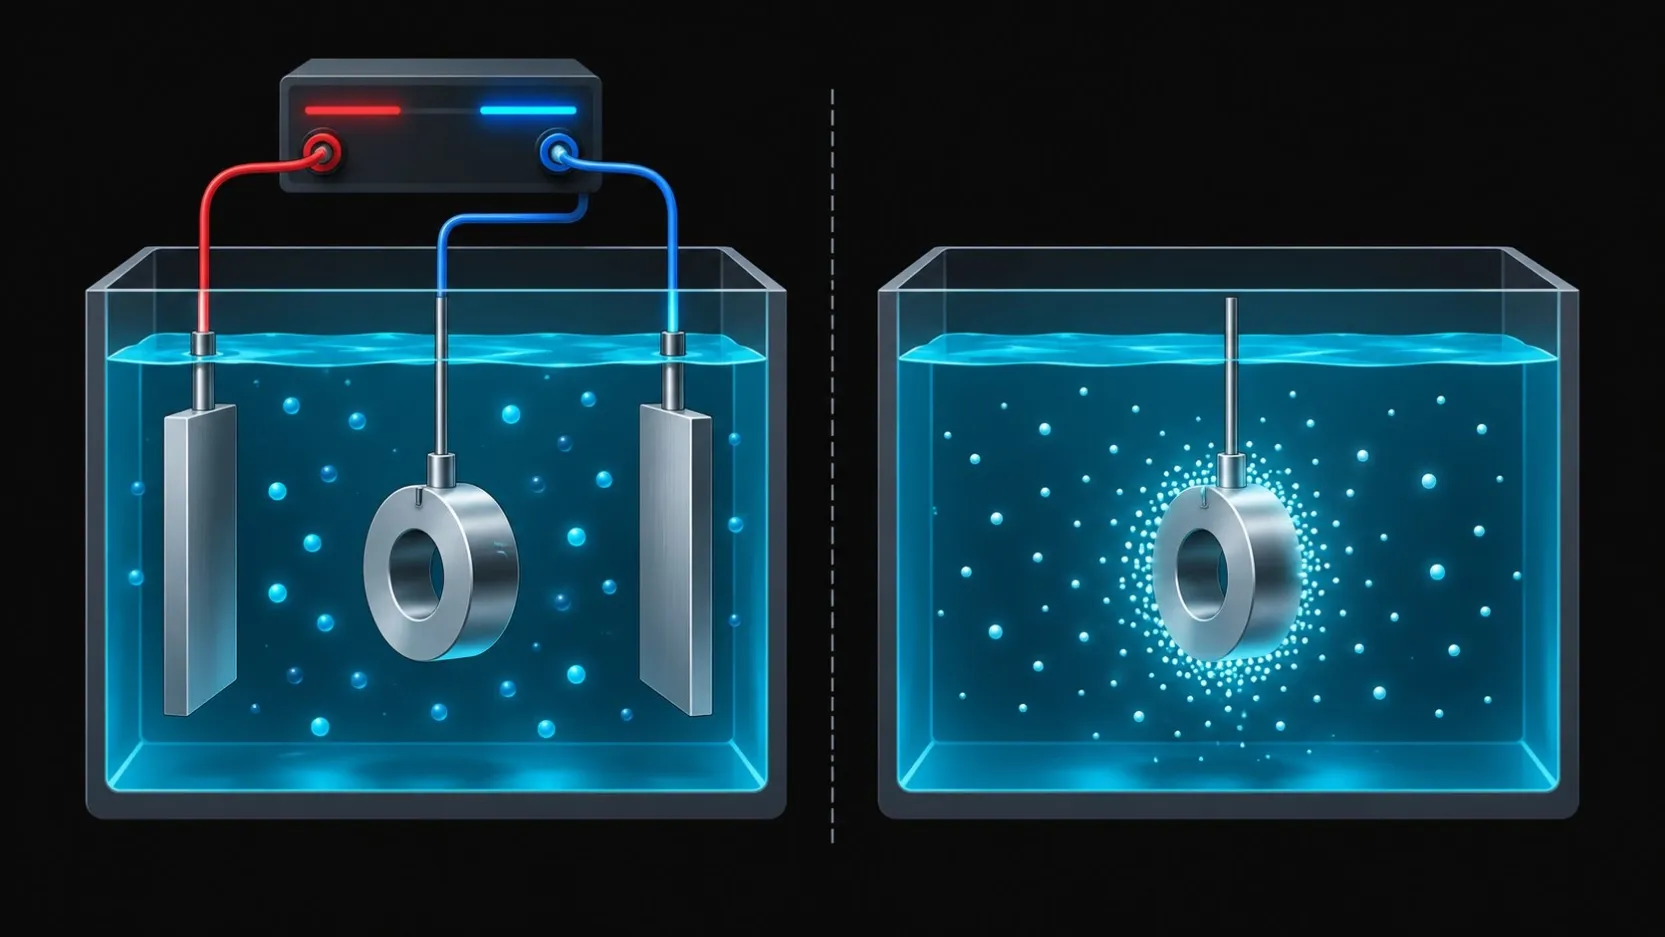
Our electrolytic versus electroless nickel comparison explains why this work belongs on an electroless line, and the thickness testing guide covers how measurement methods are chosen.
Where this does not fit
- Assumptions from an end-market label: do not add or remove an AMS requirement merely because a job sounds commercial or aerospace; actual product and customer requirements govern.
- Parts that cannot survive the class treatment: the post-plating temperature attaches to the substrate. Where the material limit and the class conflict, the specification conflict must be resolved before equipment selection.
- Substituting specifications: AMS 2404, the separate low-phosphorus AMS 2405 family and ASTM B733 address different requirements. A proposal that swaps one for another without the process owner's approval is not comparable.
- Assuming the callout equals capability: quoting a specification name proves nothing about a supplier's records. Ask for the actual evidence chain.
Questions You May Have:
Is AMS 2404 the same as ASTM B733?
No. The official ASTM B733-22 abstract describes phosphorus-composition types, service-condition numbers and post-heat-treatment classes. SAE AMS2404K covers electroless nickel-phosphorus under its own requirements. Do not translate a B733 designation into an AMS class or assume dual compliance; the contract and approved evidence decide applicability.
Which class should our drawing call out?
The design authority and process owner must choose it from the invoked edition for the substrate and required final condition. Record their approved class and treatment in the equipment brief; this article is not a replacement class-selection chart.
Why did two suppliers quote very different prices for the same callout?
Compare their assumptions about preparation, final condition, thermal processing, instruments and records. An omitted oven or inspection service can change scope, but price alone does not identify the cause.
Do we need an oven if the class is Class 1?
Check the invoked revision and all applicable treatment requirements, including substrate-related relief. Ask the process authority to define each thermal duty; a class label is not a complete oven specification.
Can an AMS 2404 project be assessed for quick turnaround?
Provide the drawing revision, substrate and incoming condition, approved process route, thermal duties, part quantity and inspection/document package. Ask which stages govern the schedule: preparation approval, plating capacity, oven/load availability, inspection or record release. A quoted tank cycle is not the complete job lead time. Any expedited schedule must retain the required treatment, tests and records; no universal quick-turn promise follows from the AMS name.
Official references
- SAE AMS2404K — Plating, Electroless Nickel-Phosphorous — official revision and public scope; the controlled contract version governs detailed clauses.
- ASTM B571 — Qualitative Adhesion Testing of Metallic Coatings — qualitative adhesion practices; applicability must be confirmed against the contract.
- ASTM B733-22 — Autocatalytic (Electroless) Nickel-Phosphorus Coatings on Metal — public abstract describing composition, service-condition and post-treatment classification.
- SAE AMS2405E — Electroless Nickel Plating, Low Phosphorus — official separate low-phosphorus scope; stabilized October 2013. It is not a substitute approval for AMS2404.
Get Proposal and Demo
Introduce your electroless nickel project with company, name, email and project country. Technical fields are optional. Provide the AMS revision, class, drawing thickness and part family when available, and request an assessment of line, oven, inspection/record interfaces and retained services. Ask for an agreed demonstration scope, such as load identification and record retrieval; availability and representative parts must be confirmed for the project.
Specifications can follow by sales email, or chat on WhatsApp. The equipment buyer's guide explains how the wider supply boundary is compared.