
Anode Spacing and Thickness Mapping in Rack Nickel Plating
Investigate uneven nickel thickness with an anode and rack map. Compare edge, recess and rack position readings before changing the electrical geometry.
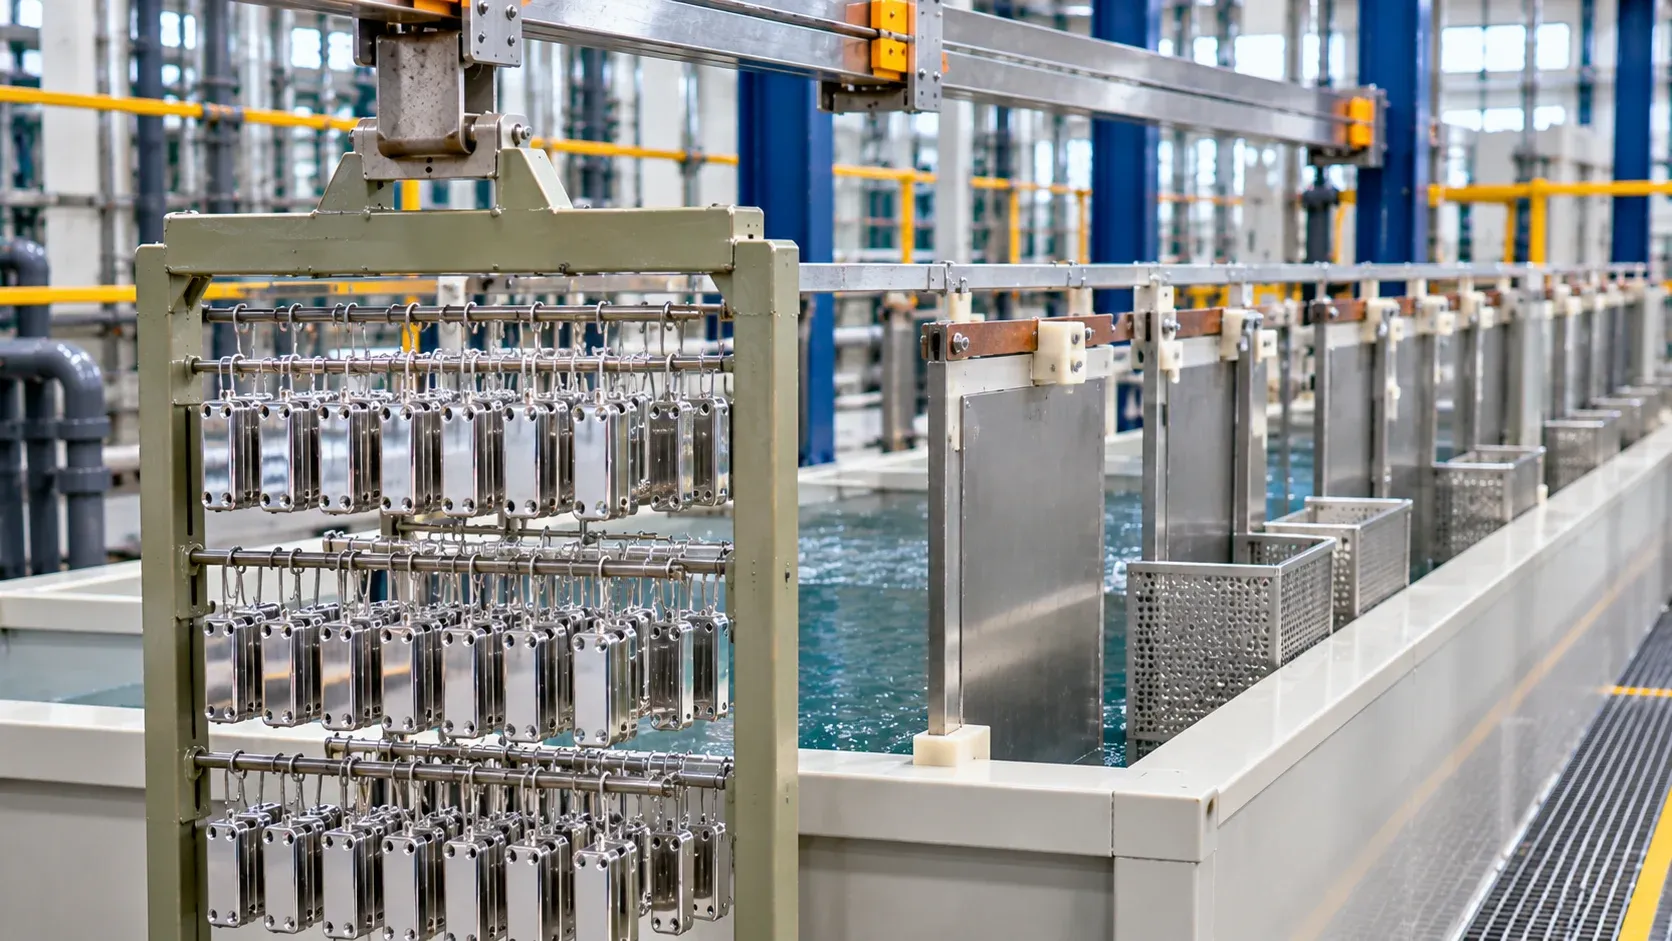
Choose anode spacing for rack nickel plating by checking thickness where the drawing requires it. Map the part and rack against the anodes, then compare edges, recesses and different rack positions. Use a controlled trial to separate a geometry problem from a change in load, contact condition or bath operation.
ES-PRO editorial team · Updated 11 November 2026
The Nickel Institute handbook explains why local thickness follows current distribution and solution behavior. Part shape, shielding and position affect the current reaching a surface. A prominence facing an anode and a recessed area on the same part can receive different deposits.
Draw the electrical geometry at the loaded position
Make a plan and side view showing the anodes, cathode rack and loaded parts. Mark the fixture revision and which positions are occupied. Record distance from the relevant anode faces to the named part features at the production position. Include orientation and any shield or auxiliary anode in the drawing. Keep the map consistent when comparing trials.
Note what else can affect the result: part surface area, the condition of contacts and anodes, the approved bath window and electrical program, and the time the load spends at the station. Ask the process owner to confirm which of these stayed comparable. Position alone cannot explain a difference if the two racks also used different programs or bath conditions.
Thickness pattern | Comparison to make | Candidate response to evaluate |
|---|---|---|
Edge high and recess low across rack positions | Compare the same part feature across racks | Review orientation and electrical geometry with the process owner |
Low readings at one rack position | Move matched parts through the affected and reference positions | Check contacts, neighboring parts and local anode conditions |
Different results on anode-facing and shaded faces | Confirm face orientation and measurement method | Evaluate how the part faces the anodes at the qualified load |
All positions shift between runs | Compare route, current program, bath record and measurement checks | Resolve the overall change before drawing a geometry conclusion |
Worked example with a nickel-plated recessed bracket
Suppose both outer faces meet the drawing but a recessed seat repeatedly reads low. Record the thickness method and verify that the reading represents the actual seat. Then measure the same seat and an outer reference face on parts at the rack center and edge. If the seat is low at every position, investigate the feature and electrical path. If the result follows a rack position, investigate what differs at that location.
Trial one approved change at a time where possible. An orientation change may alter drainage or neighbor clearance, so repeat the relevant handling checks as well. A shield may redistribute current and change readings on other faces. An auxiliary anode introduces its own support, connection and maintenance requirements. Have the process owner define the safe trial configuration and electrical conditions.
The result that matters is the whole measurement map. Confirm the critical seat without moving another surface outside its acceptance requirement. Repeat on a representative load and record the configuration the equipment must reproduce.
Separate a part effect from a position effect
Use comparable parts from the same incoming lot. Mark their critical points before the run. Put one set in the suspect position and one in a reference position. In a repeat run, exchange equivalent parts between those positions while retaining the approved load pattern. Compare results by both feature and position. A recurring low point on the same feature and a recurring low rack position lead to different follow-up checks.
Keep the raw readings as well as the pass decision. A position can remain inside specification while moving closer to a limit. That trend can justify another comparison before the geometry becomes the production reference.
Turn the map into a line requirement
Supply the rack and part drawings, annotated critical measurement locations, anode arrangement and accepted range of load patterns. If the project needs an adjustable or removable feature, define which positions are usable and who controls adjustments. Ask for practical access for inspection and replacement.
Use the coating thickness measurement guide to discuss method access and the rectifier selection guide to connect the validated load to the electrical brief. Record trial ID · rack position · feature · distance and orientation · fixture revision · current program · reading and method · decision.
Where the trial uses baskets and bags, link their arrangement and access requirements to the anode basket and bag guide.
FAQ
Is there a universal anode-to-part distance?
Use the approved process and the measured thickness map for the actual geometry, load and bath.
Will more current solve a thin recess?
Review the local distribution and critical surfaces first. A total current change can change several locations at once.
Does the drawing's average thickness prove the recess meets its minimum?
Use the inspection locations and acceptance criteria required by the controlling drawing or specification.
Discuss a nickel plating thickness map
Share your rack drawing and measurement locations. Include the part family, load and observed readings. Send drawings by sales email, or discuss the project on WhatsApp.
Image note: AI-generated editorial photography illustrates equipment or workpiece contexts; it is not an ES-PRO installation, customer reference or evidence of coating performance.


