
Plating Process
Electropolishing or Mechanical Polishing for Stainless?
Compare electropolishing and mechanical polishing by surface function, feature access and final dimensions. Plan a representative trial and inspection map.
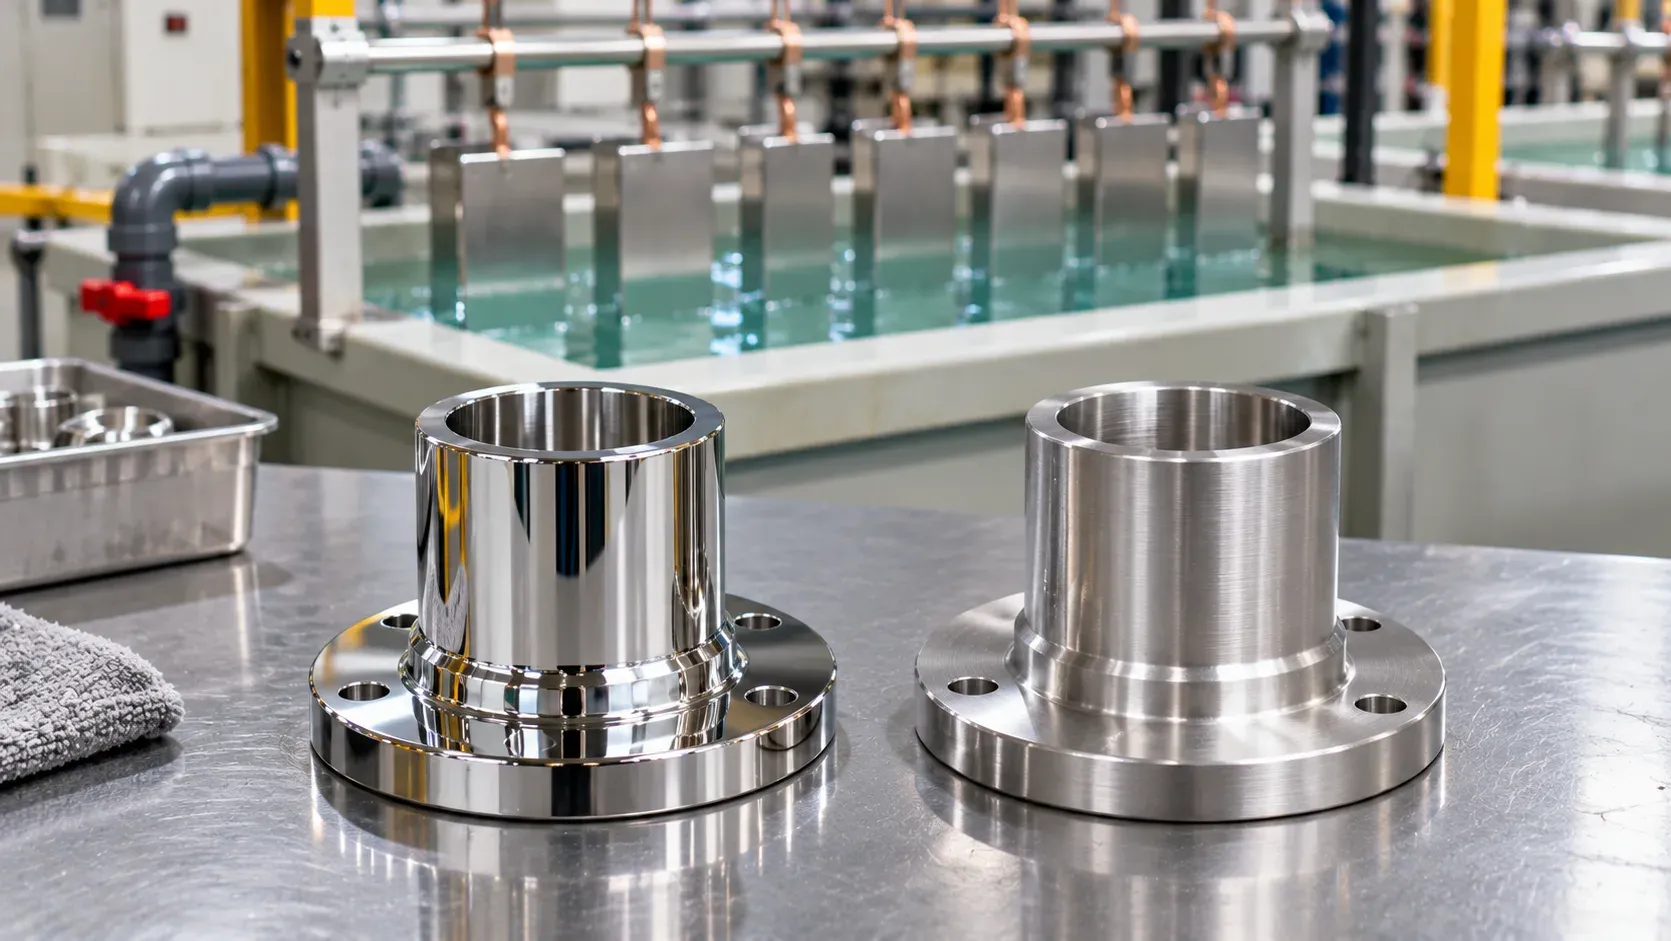
Stainless steel parts often need more than a clean surface: they need one that resists corrosion in aggressive media, sheds bacteria, and stays bright under inspection lights. Electropolishing delivers that — but only when the line is engineered for it. This guide compares electropolishing with mechanical polishing across the decisions that matter, quantifies what each removes, and ends with the equipment scope for a stainless electropolishing line.
Written for buyers planning capacity — a planning document, not a process datasheet. Confirm exact parameters with your chemistry supplier.
The four finishing routes, side by side
Buyers searching this topic usually compare electropolishing against three alternatives. The right choice depends on what the surface must do:
Route | Mechanism | What it changes | Best for |
|---|---|---|---|
Electropolishing | Electrolytic removal — the part is the anode; micro-peaks dissolve preferentially | Surface topography and chemistry: removes free iron, enriches chromium oxide layer | |
Mechanical polishing | Abrasive removal — wheels, belts and compounds cut the surface | Surface topography only; can smear metal and leave abrasive embedment | |
Passivation | Chemical treatment — acid bath removes free iron without changing topography | Chemistry only: restores the passive layer on an existing surface | |
Electroplating | Electrolytic deposition — adds a metal layer on top | Adds material: changes dimensions, appearance and properties |
The key distinction buyers miss: passivation changes chemistry without touching geometry; electropolishing changes both; electroplating adds material. A part that needs corrosion resistance AND a smooth, featureless surface needs electropolishing — passivation alone leaves machining marks, mechanical polishing leaves embedded abrasive.
How much material does each remove?
Material removal is where the routes separate quantitatively:
Route | Typical removal | Dimensional impact |
|---|---|---|
Electropolishing (deburring pass) | As little as 0.0025 mm (0.0001") | Negligible — safe for tight-tolerance parts |
Electropolishing (full bright pass) | 5–20% of the removal that mechanical polishing would need for the same finish | Small but must be included in tolerance stacks |
Mechanical polishing | 0.008–0.018 mm (0.0003–0.0007") typical | Significant — plan tolerance allowance |
Because electropolishing removes so little material, it suits parts with tight tolerances — medical devices, seals faces, precision fittings — where mechanical polishing would take the part out of spec.
Where electropolishing wins — and where it cannot help
Honest limitations first, because they prevent wasted quotes:
- Visible machining marks survive. Electropolishing smooths micro-peaks (the sub-micron texture), but deep tool marks and scratches remain — they are geometry, not roughness. Parts needing scratch removal need mechanical polishing first, then electropolishing as the final step.
- Magnetic stainless grades are unsuitable. Free-machining and magnetic stainless variants do not respond to electropolishing — the chemistry and current distribution do not produce the desired dissolution. Confirm the grade before quoting.
- Foreign inclusions show up. Embedded particles from prior mechanical work can become visible after electropolishing.
Where it wins, it wins decisively: removing free iron contamination from the surface (the main trigger of premature rust on stainless), reducing residual stress from machining, lowering the risk of stress-corrosion cracking, and producing the bright, ultra-clean, passivated surface that medical, pharmaceutical, food and semiconductor applications specify.
Industries that specify electropolishing
The specification appears wherever cleanability and corrosion resistance are audited: medical devices and instruments, pharmaceutical process equipment, food and beverage plant components, aerospace hydraulics, semiconductor and electronics parts, and automotive fuel and brake components. Each industry adds its own surface-verification requirements — which is where process documentation earns its keep.
The equipment scope for a stainless electropolishing line
Electropolishing is electroplating's mirror image: the same power and control infrastructure, with the part at the anode. The line scope includes:
Item | Specification points |
|---|---|
Electrolyte tank and chemistry | Phosphoric-sulfuric electrolyte system per supplier specification; heating and temperature control; agitation |
Rectifier and busbars | DC rectifier sized to current density × loaded area; cathode bars and contacts |
Racking and contacts | Part-specific anode racks with fixed contact points — contact marks must land on non-critical faces |
Rinse and neutralization | Counterflow rinsing, neutralization stage, and the effluent treatment the electrolyte requires |
Fume control | Extraction over the tank — electropolishing evolves gas at the anode |
Records | Current density, time and temperature logging per batch for process evidence |
The rectifier sizing method follows the same logic as plating: see the surface area and rectifier load guide. Racking and contact-mark planning is in the masking and loading guide; effluent treatment for the electrolyte stream in the wastewater treatment brief.
Key takeaways
- Passivation changes chemistry; electropolishing changes chemistry AND geometry; electroplating adds material — pick by what the part needs.
- Electropolishing removes as little as 0.0025 mm on deburring passes — safe for tight tolerances where mechanical polishing is not.
- Deep machining marks survive electropolishing: sequence mechanical polishing first when scratch removal is required.
- Magnetic stainless grades cannot be electropolished — confirm the grade before quoting.
- The equipment scope mirrors a plating line: rectifier, racks, rinsing, effluent treatment and batch records.
Your next five steps
- Confirm the stainless grade and whether electropolishing applies to it.
- Decide the sequence: mechanical pre-polish where scratches must go, electropolish last.
- Size the rectifier against loaded surface area and current density.
- Specify racking so contact marks land on non-critical faces.
- Add the effluent treatment scope for the electrolyte stream.
FAQ
How is electropolishing different from passivation?
Passivation is a chemical treatment that removes free iron and restores the passive layer without changing surface geometry. Electropolishing electrochemically removes a thin layer of metal, changing both chemistry and topography. Many stainless specs call for electropolishing followed by passivation.
How is it different from electroplating?
Electropolishing removes material (the part is the anode); electroplating deposits it (the part is the cathode). The equipment infrastructure is similar, which is why both lines often share a hall.
Can electropolishing remove deep scratches?
No — it smooths micro-texture, not geometry. Deep marks need mechanical polishing first; electropolishing then brightens and passivates the polished surface.
Image note: AI-generated editorial photography illustrates equipment or workpiece contexts; it is not an ES-PRO installation, customer reference or evidence of coating performance.


