
Plating Process
Electroless Nickel Properties Equipment
Electroless nickel plating (ENP) is an autocatalytic process — no rectifier, no anodes, no current density distribution issues. The nickel-phosphorus deposit is chemically deposited and grows uniforml
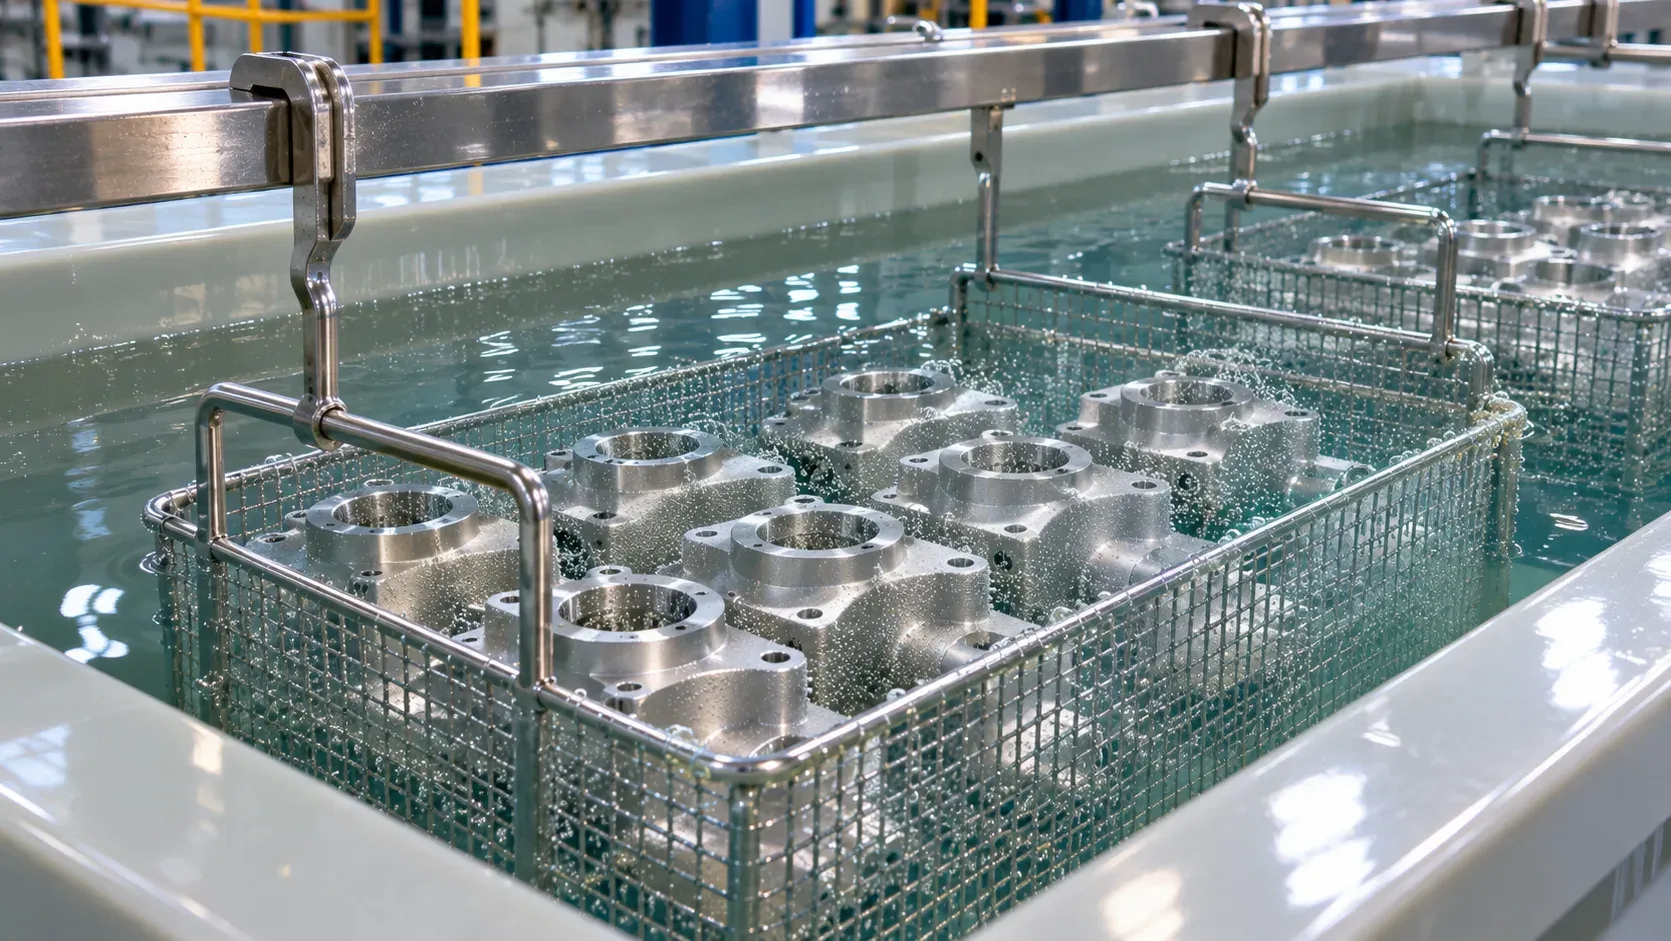
Electroless nickel plating (ENP) is an autocatalytic process — no rectifier, no anodes, no current density distribution issues. The nickel-phosphorus deposit is chemically deposited and grows uniformly on every surface the solution touches, including blind holes, threads and internal channels. This uniformity is the process's defining advantage, and it changes the equipment scope fundamentally compared with electrolytic plating.
Technical planning document — confirm chemistry parameters (temperature, pH, phosphorus content) with your chemistry supplier.
The deposit properties that drive the specification
Property | Low-P (< 5% P) | Mid-P (5–8% P) | High-P (> 9% P) |
|---|---|---|---|
As-deposited hardness | 600–700 HV | 500–600 HV | 450–550 HV |
After heat treatment (400°C) | 900–1100 HV | 850–950 HV | 900–1000 HV |
Corrosion resistance | Moderate | Good | Excellent (best for aggressive media) |
Magnetic | Magnetic | Weakly magnetic | Non-magnetic |
Best for | Wear resistance, repair | General engineering | Corrosion protection, electronics |
The phosphorus content is the specification decision that drives the equipment scope — higher phosphorus chemistry requires different operating temperature, pH and stabiliser additives.
The equipment scope: what differs from electrolytic plating
Item | Electroless nickel | Electrolytic nickel |
|---|---|---|
Power supply | None — no rectifier needed | DC rectifier sized to loaded area |
Anodes | None — the chemistry does the work | Nickel anodes or insoluble anodes |
Current distribution | Not applicable — deposit is uniform on all surfaces | Current density distribution determines deposit thickness |
Tank material | PP or 316L stainless (nickel plates on rough surfaces — smooth tank interior prevents plate-out) | PP or stainless |
Temperature control | Critical — 85–92°C ± 2°C; heating system required | 45–60°C ± 3°C |
pH control | Critical — pH affects deposition rate and phosphorus content | pH is less critical |
Stabiliser dosing | Continuous stabiliser addition prevents tank plate-out | Not applicable |
Filtration | Continuous filtration through 1–5 µm — removes particulate nucleation sites | Standard filtration |
Tank liner or passivation | Nitric acid passivation of the tank between batches to prevent plate-out | Not applicable |
The temperature and pH control are the most critical equipment items — electroless nickel is sensitive to both, and deviations cause batch failure or tank plate-out. Specify redundant heaters and pH monitoring with alarm.
Key takeaways
- No rectifier, no anodes, no current density issues — uniform deposit on every surface.
- Phosphorus content (low/mid/high) is the specification decision that drives properties.
- Temperature control at 85–92°C ± 2°C and pH control are the most critical equipment items.
- Tank plate-out prevention (smooth walls, stabiliser, passivation) is a unique equipment concern.
- High-phosphorus ENP is the best corrosion protection; low-phosphorus is the best wear resistance after heat treatment.
Your next five steps
- Define the phosphorus content based on the deposit properties your application needs.
- Specify redundant temperature control and pH monitoring for the ENP bath.
- Design the tank with smooth interior walls to minimise plate-out.
- Plan the nitric acid passivation routine between production batches.
- Add continuous filtration to prevent particulate nucleation sites.
FAQ
Can we plate aluminum with electroless nickel without a strike?
Yes — aluminum needs a zincate pre-treatment (double zincate for some alloys) before ENP. The ENP itself does not require electroplating-style activation. The zincate scope is separate.
Why does our ENP tank plate out on the walls?
Plate-out occurs when the solution becomes unstable — typically from temperature overshoot, pH drift, insufficient stabiliser, or rough tank walls that provide nucleation sites. Smooth tank walls, stabiliser dosing and tight temperature control prevent this.
Is heat treatment always needed after ENP?
Only if increased hardness is required. Heat treatment at 400°C for 1 hour transforms the nickel-phosphorus deposit, increasing hardness from 500 HV to 900–1100 HV. For corrosion applications, as-deposited (unheated) ENP provides better corrosion resistance.
Image note: AI-generated editorial photography illustrates equipment or workpiece contexts; it is not an ES-PRO installation, customer reference or evidence of coating performance.


